MY CORLISS
ENGINE BUILD
Part six by Vince Cutajar



MY CORLISS
ENGINE BUILD
Part six by Vince Cutajar


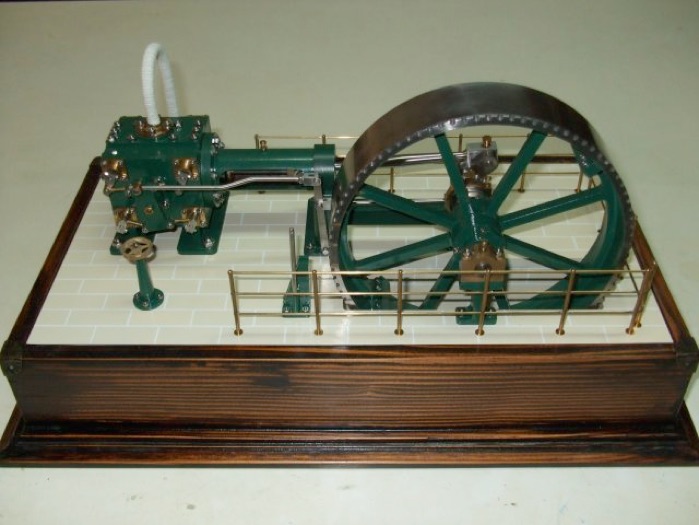
The eccentric strap was ready to mill and rough out with step milling.
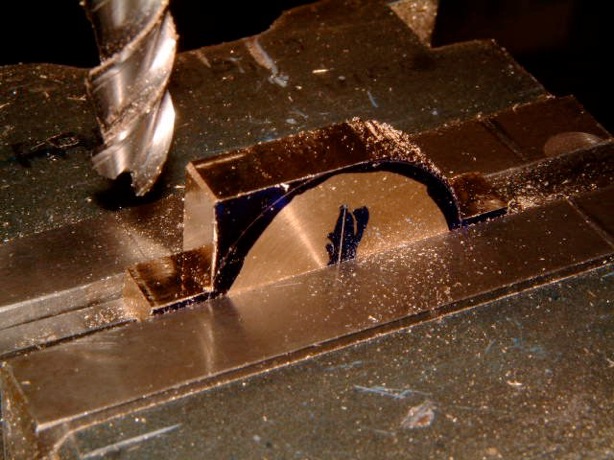
And here are both sides roughed out.
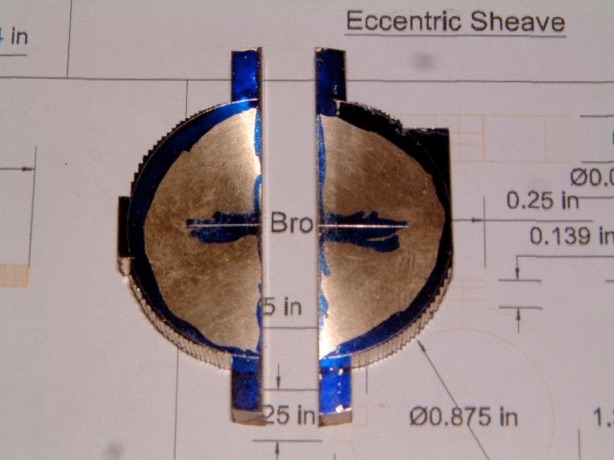
Clamped them together in the vice and drilled the two 2mm holes for the bolts.
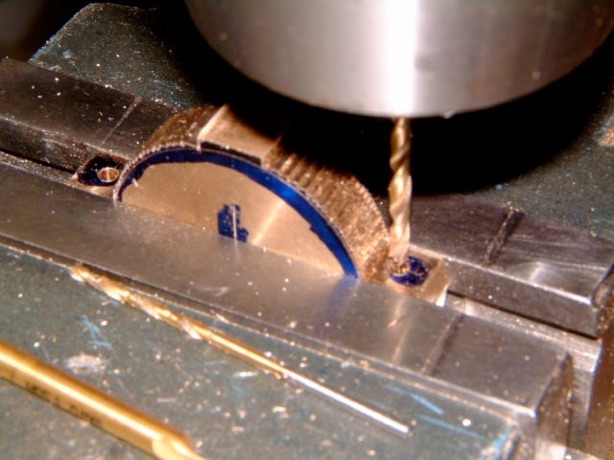
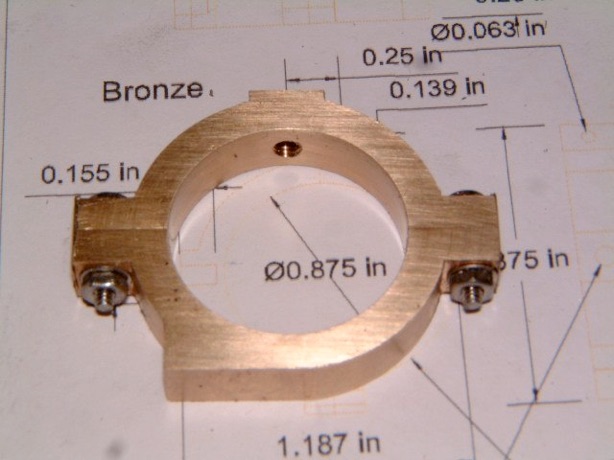
And here it is bolted together. Fiddly little things those 2mm nuts and thin nuts.
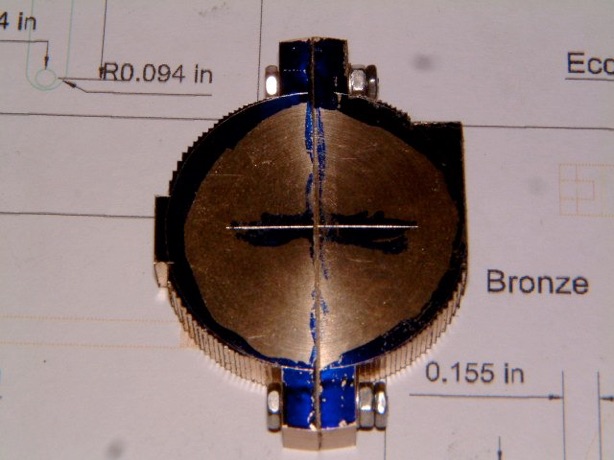
I bored out the eccentric strap.
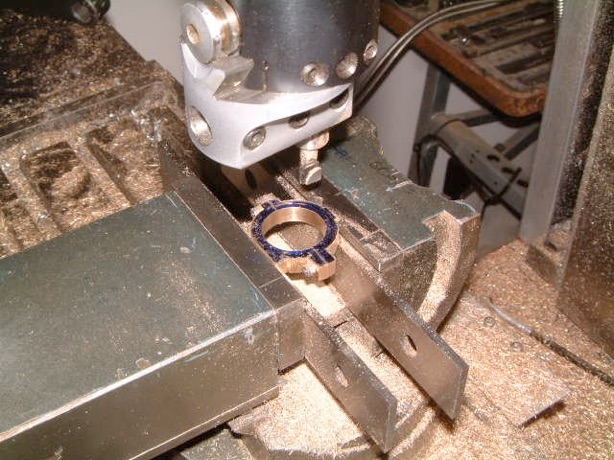
I made a mandrel so that I can solidly hold the eccentric in the rotary table and clocked it up.
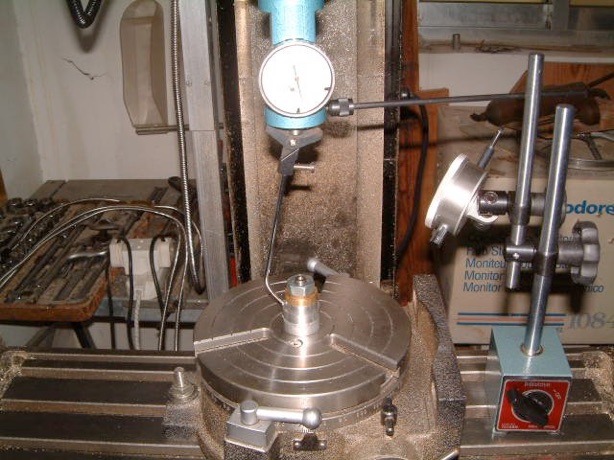
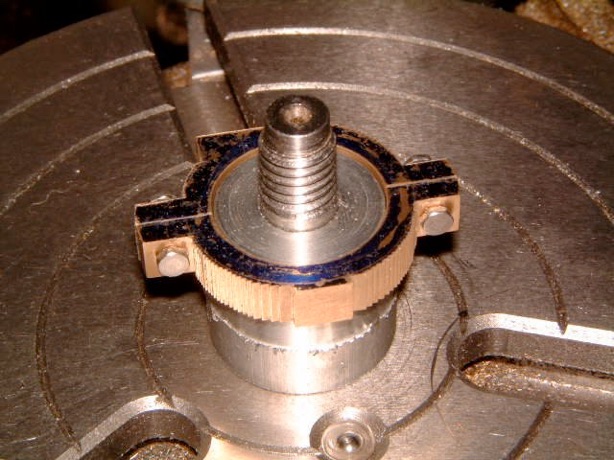
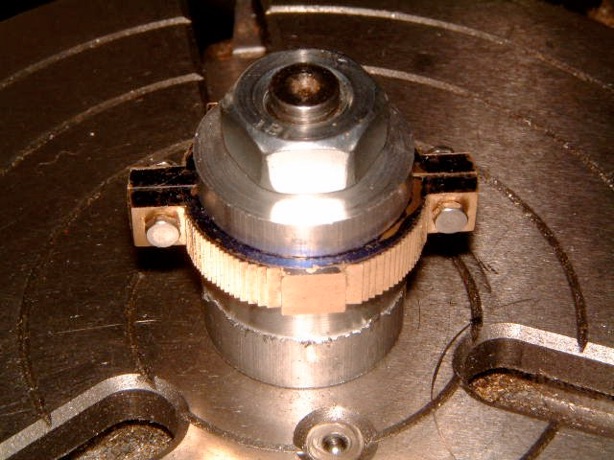
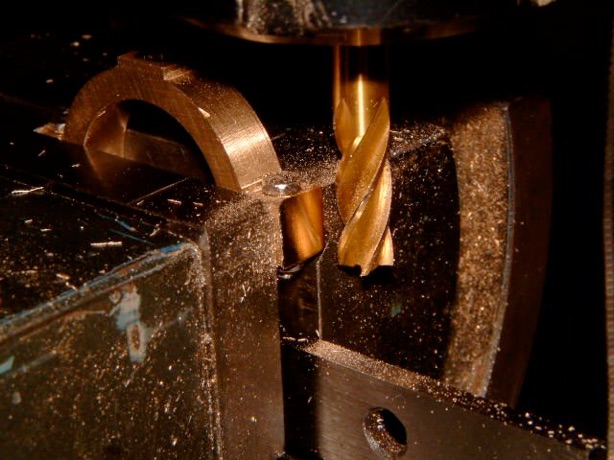
Then I started cleaning up the outside of the strap with a 3mm endmill
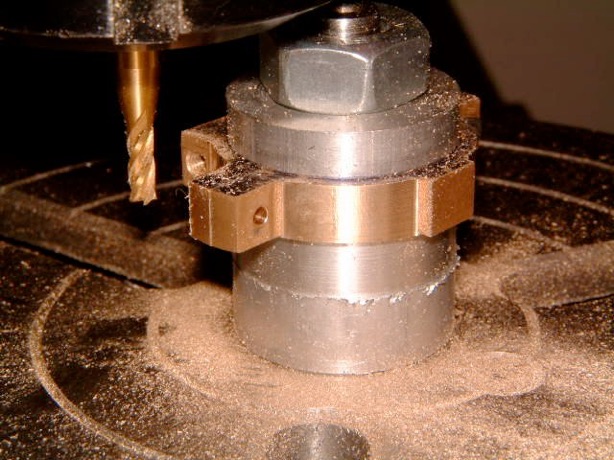
Then cleaned up the sides of the mounting lugs.
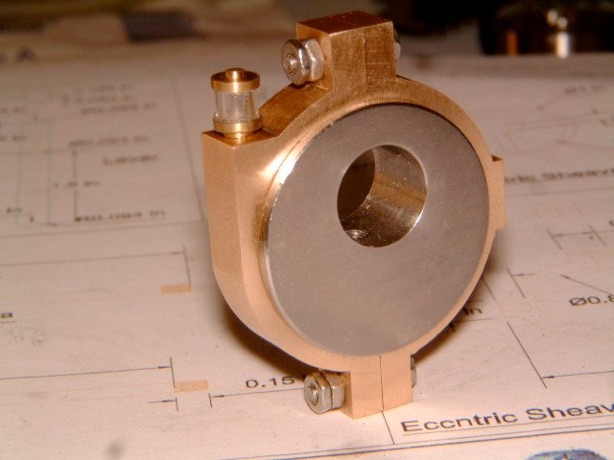
The 3mm tapped hole for the eccentric rod was made. All that remains is to drill for the oil hole and then give it a good deburr and clean up.
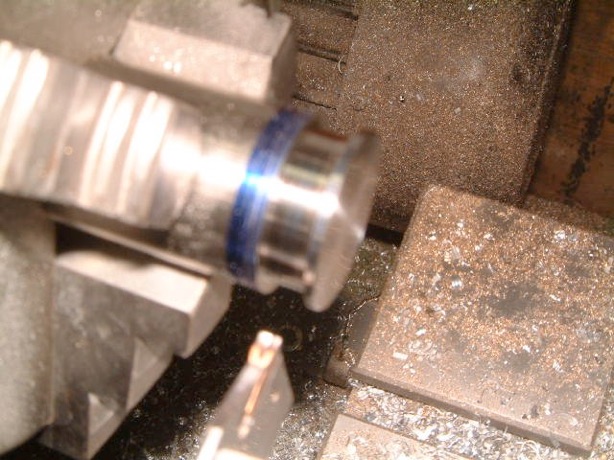
For the eccentric sheave, the only material I had in 1" diameter was 316 stainless. I was a bit hesitant in using it as I have seen many people complain that it is not that easy to work with. But that is what I had and decided that might as well give it a try. Chucked a piece in the lathe and to be sure used a new insert in my Q-cut parting tool.
The tool complained a bit until I found the correct pressure to apply. Made the groove about 0.5mm oversize and then with small cuts moved the parting tool sideways in the groove to get close to the desired depth. Then it was slowly fitted to the strap using emery paper.
Off to the mill, the off-centre hole was drilled and reamed.
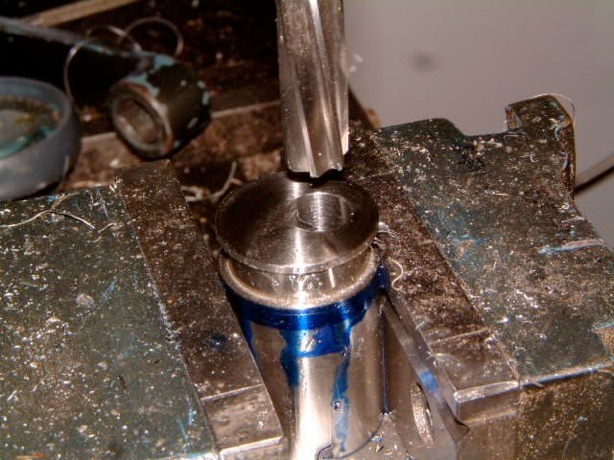
The 3mm tapped hole for the grub screw was made next (was extra careful during tapping) and the piece was again taken to the lathe where it was parted off and cleaned up.
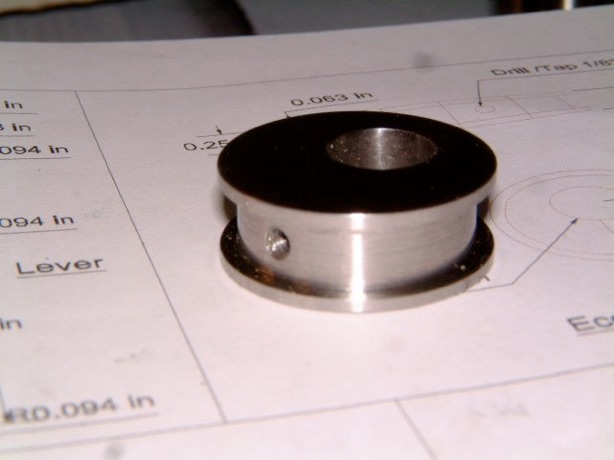
Well, it was a positive experience machining 316 stainless. Here’s the finished eccentric:

Modelengineeringwebsite.com
the only free and the only weekly magazine for model engineers.
Editor: David Carpenter