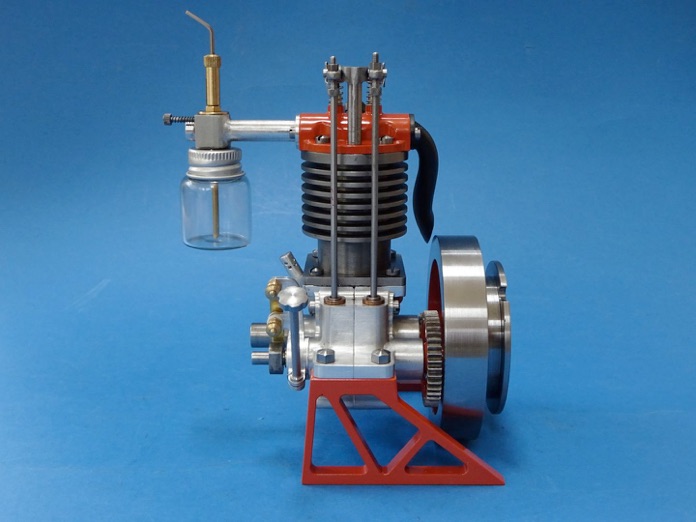


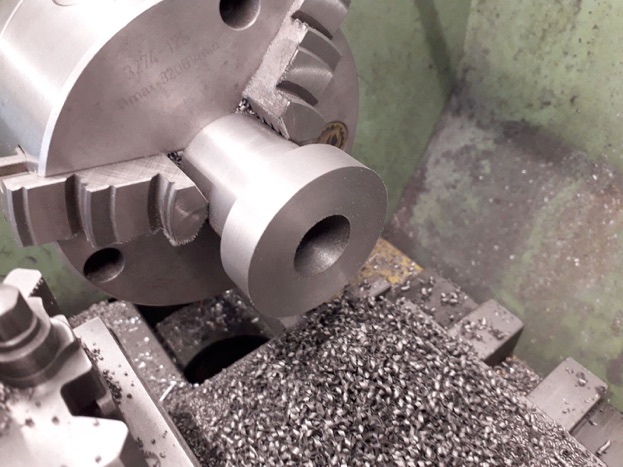
A piece of cast iron for the cylinder was turned down to the diameter of the fins and then held by this reduced diameter to face the end and bore out to 24mm,
before cutting a spigot on the end to locate in the crankcase.
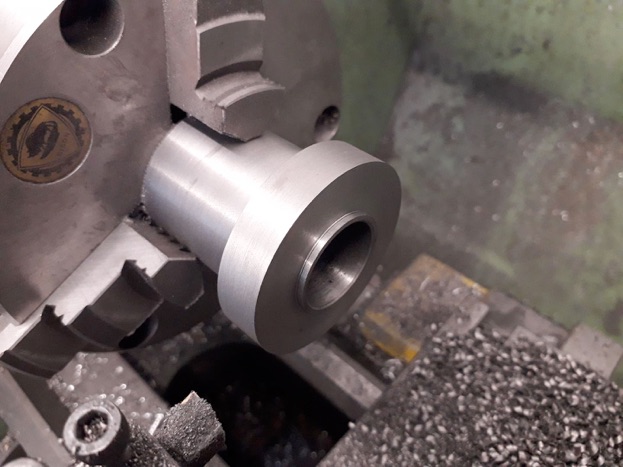
Like a lot of parts I make, one was used to gauge the size of the other. This fit was about right.
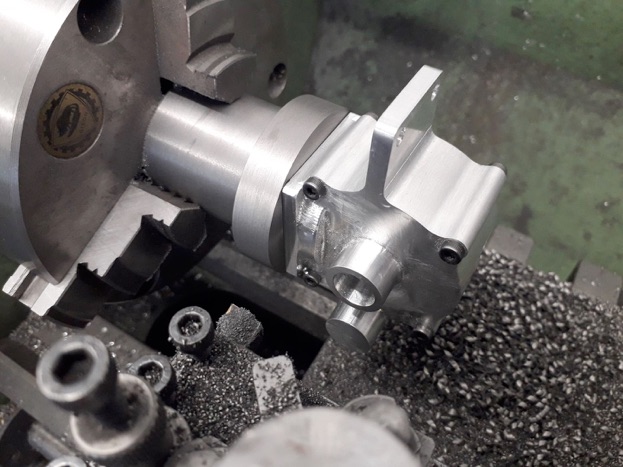
The cylinder was again reversed in the chuck and with tailstock support the slots between the fins were added with an insert parting tool
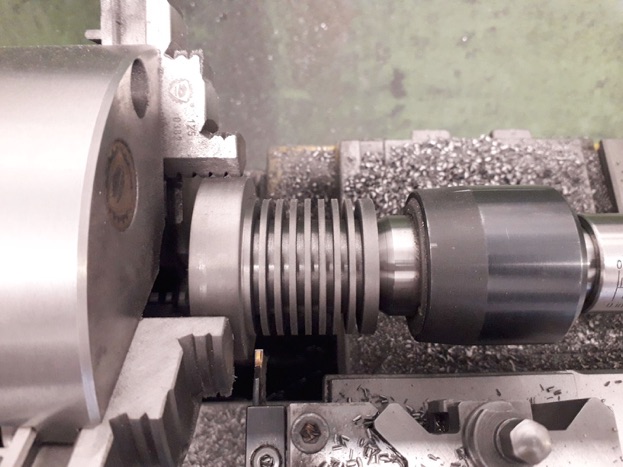
The last turning job now that I did not need anything too solid to hold by was to machine the waist between fins and mounting flange
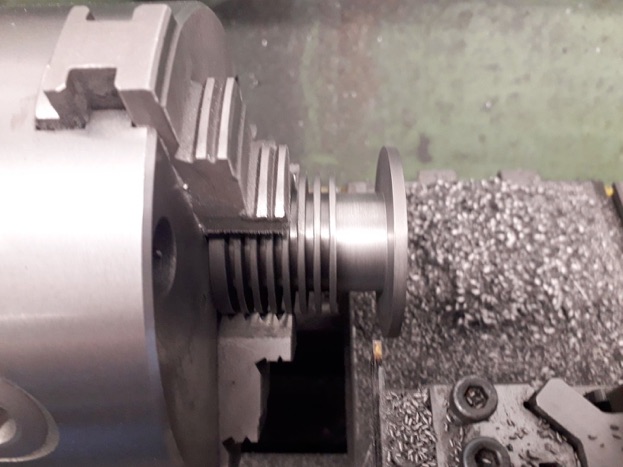
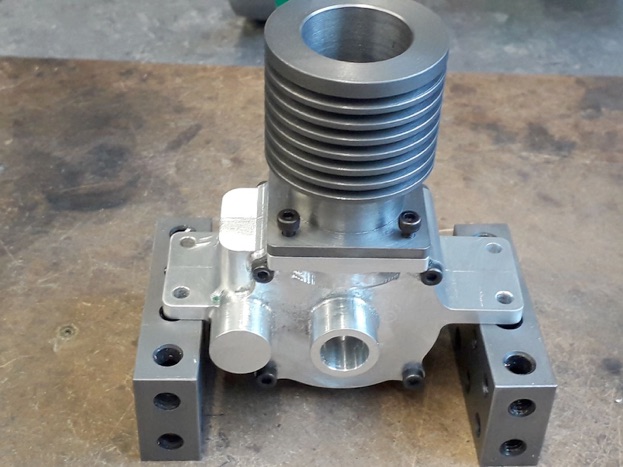
As I wanted the practice on the CNC I used that to give the flange its square shape with rounded corners and also drill the mounting holes.
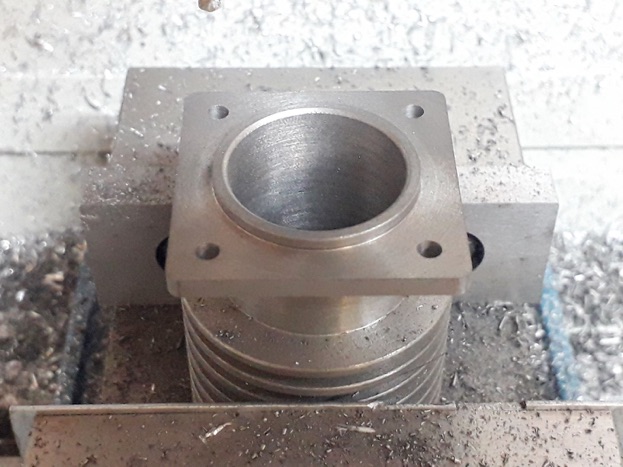
That gave me an excuse for a test fit.
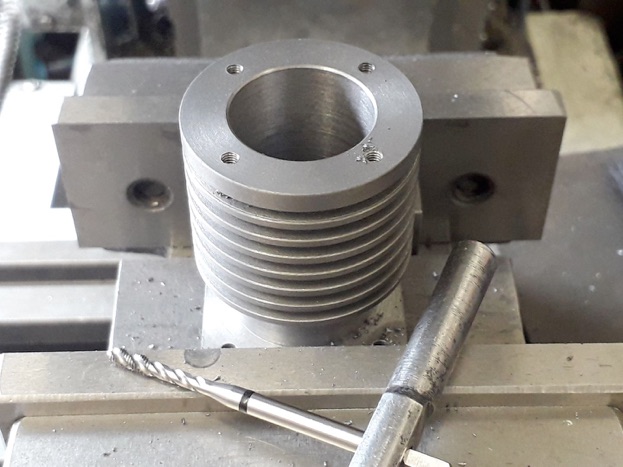
The last machining job on the cylinder was drilling and tapping for the head fixings, the spiral flute taps work just as well on crumbly materials as those that produce long swarf. Just needs a bit of honing to complete.
Part one here Part two Part three Part four Part five Part six Part seven