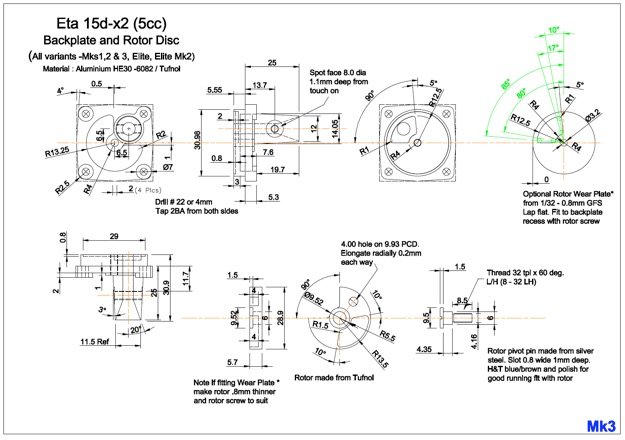


The backplates began as 35mm long blocks of 38 mm square HE30 Aluminium. First off was to bring them square and 1mm up on all faces and centre drill for the venturi position and the register on the opposite face.

The intake hole was drilled and the taper turned then the block reversed for turning the register and recess for the rotor plate. The red blocks are 6mm perspex which makes for very good protective packing.

Next up was to press that previously made drill jig into service and drill the bolt holes.

Then set the blocks up on the rotary table for milling the intake cavity. This shows the leading and trailing edges being defined (important) - before removing the waste - (not so important).

Next up was to rough out around the intake tube then set them up in a clamp plate on the face plate for finishing to thickness and turning the taper on the intake tube OD.

With that done the plate was transferred to the rotary table on the mill for roughing and finish milling the pocket in the back.

The bolt bosses were milled - note the pin for indexing rather than setting up each hole.


After a good initial fettling and smoothing with Scotchbrite and Garryflex that clamp plate was pressed into service once more for cross drilling and tapping the 2BA holes for the spray bar

And again for milling the side angles

And yet again for milling the clearance for the bolt head in the intake tube.

After another fettling they ended up like this.

See part one here part two part three part four part five part six part seven part eight
part nine part 10 part 11 part 12 part 13 part 14 part 15 part 16